When Colour Drifts During Production: Check Masterbatch Dosing Before Changing the Formulation
Colour variation during a production run is often blamed on the masterbatch first. Sometimes the formulation is involved, but changing colourant before checking the dosing system can hide the actual cause and create a second variable. A controlled investigation starts by asking whether the same proportion of masterbatch reached the melt throughout the run.
Stable colour depends on more than the percentage entered on a controller. Feeder calibration, material flow, bulk-density changes, bridging, machine throughput, mixing and the timing of sample collection can all change the effective addition rate seen by the process.
Start with a time-based sample sequence
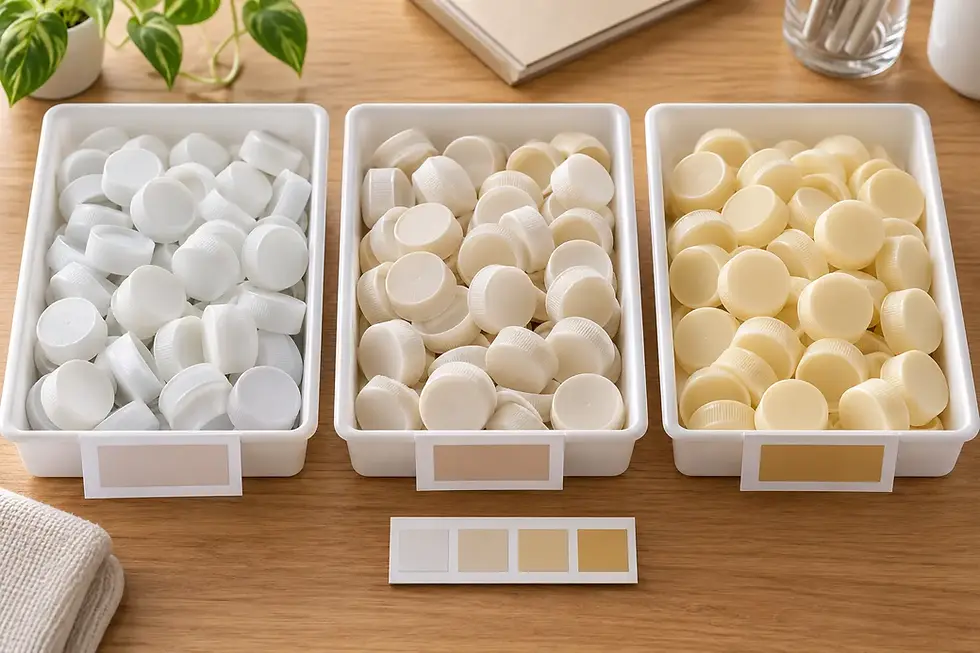
Collect labelled samples from the start, middle and end of the run, then record the machine settings, material batch references and feeder readings. This distinguishes a steady offset from progressive drift. A steady offset may point to an incorrect setpoint, wrong material or colour-standard mismatch; gradual change directs attention toward dosing stability, throughput, residence time or thermal conditions.
Confirm the calculation behind the setpoint
Confirm what the displayed percentage means in the specific dosing system. Depending on the setup, the target may be entered relative to the natural resin, total blend weight, shot weight or extrusion throughput. A correct number entered against the wrong basis produces a repeatable error. Check the approved recipe, actual shot weight or measured line output and the intended let-down ratio. Where regrind is present, confirm that the control calculation includes it correctly.
Recalibrate after material or setup changes
Volumetric feeders deliver material according to volume and time. Output can change when pellet geometry, bulk density or flow behaviour changes, even if screw speed is unchanged. Recalibration is important after a masterbatch change, feeder clean-out, screw change or significant production-rate change.
Gravimetric loss-in-weight systems measure mass and can correct feed rate when delivery moves away from the setpoint. They still require correct installation and configuration, plus attention to refill events, vibration, blocked flow and maintenance. The practical question is whether actual delivered mass has been checked under the current job conditions.
Look for interrupted or uneven flow
A feeder may average the correct quantity over a long interval while still delivering it unevenly. Hopper bridging, worn dosing components, intermittent refill, material build-up, static, vibration or an unsuitable screw can create pulses or gaps. Short-cycle moulding and low addition rates are particularly sensitive because each shot contains only a small mass of masterbatch.
Compare dosing with actual machine throughput
In extrusion, a feeder set against an assumed line rate can underdose or overdose when main throughput changes. In injection moulding, an incorrect shot-weight entry, cycle interruption or change in recovery conditions can alter the relationship between colour feed and resin consumption. Record actual output rather than relying only on a nominal setting. If the process permits, compare delivered masterbatch with consumed base resin over a defined interval, following the equipment supplier's safety instructions.
Control mixing and colour inspection
Correct average dosage does not guarantee a uniform part if materials separate before reaching the screw or if mixing is weak. Differences in pellet size, shape, surface condition or conveying behaviour can contribute to segregation. Hopper level, loading method and long transfer paths may also affect consistency.
Compare representative parts using the same resin, wall thickness, surface texture, conditioning time and lighting. A hot part beside a cool reference may appear different even when the material is unchanged.

A practical troubleshooting order
Label samples from defined times in the run.
Confirm the masterbatch and resin batch references.
Verify the dosage basis, setpoint, shot weight or measured throughput.
Check feeder calibration and actual mass delivery.
Inspect for bridging, refill disturbance, wear, build-up or interrupted flow.
Review mixing, conveying and possible segregation.
Compare parts under agreed lighting after consistent conditioning.
Change one controlled variable at a time and retain the results.
When a formulation review is appropriate
If dosing and process checks are stable but the approved colour is still not achieved, review the masterbatch against the actual polymer, part thickness, surface finish and processing window. Carrier compatibility, pigment selection, dispersion and heat history may all influence the final appearance.
Corbi Polymer (Sepidar Branch) can support processors with application-specific masterbatch selection and structured production-trial evaluation. Share the polymer grade, process, intended dosage, part geometry, colour target, operating conditions and representative samples so the discussion begins with the real application rather than a nominal colour code alone.


Comments